The trouble you’ll face at the gate
Suppliers promise throughput and safety as if both were simple weather to predict, and that’s where you stumble. You need to know whether a prismatic pack line really runs to spec or whether it’s been shoehorned from a blade battery assembly line with hopes and glue. I’ve stood on factory floors in Dublin and Shenzhen and seen the same signs: neat brochures, hurried acceptance tests, and instruments that look impressive until someone asks for raw logs. Somewhere in the same breath you’ll hear claims about a blade battery alternative — that’s useful context, but what you need is measurable proof, not a story.
Attack the problems, one by one
Begin with specific failure modes and match them to processes. Prismatic packs hide mechanical stress points at welds and junctions; thermal paths differ from cylindrical cells. Ask concrete questions and demand concrete answers:- Can the supplier show weld-cross-section images and failure-mode analyses from their own line?- What are the cycle times for cell insertion, welding, and potting, and how were those times measured?- How do they control torque and pressure for mechanical joins across shifts?If they can’t hand you a single real measurement, they’re running on hope.
Factory verification — what to inspect
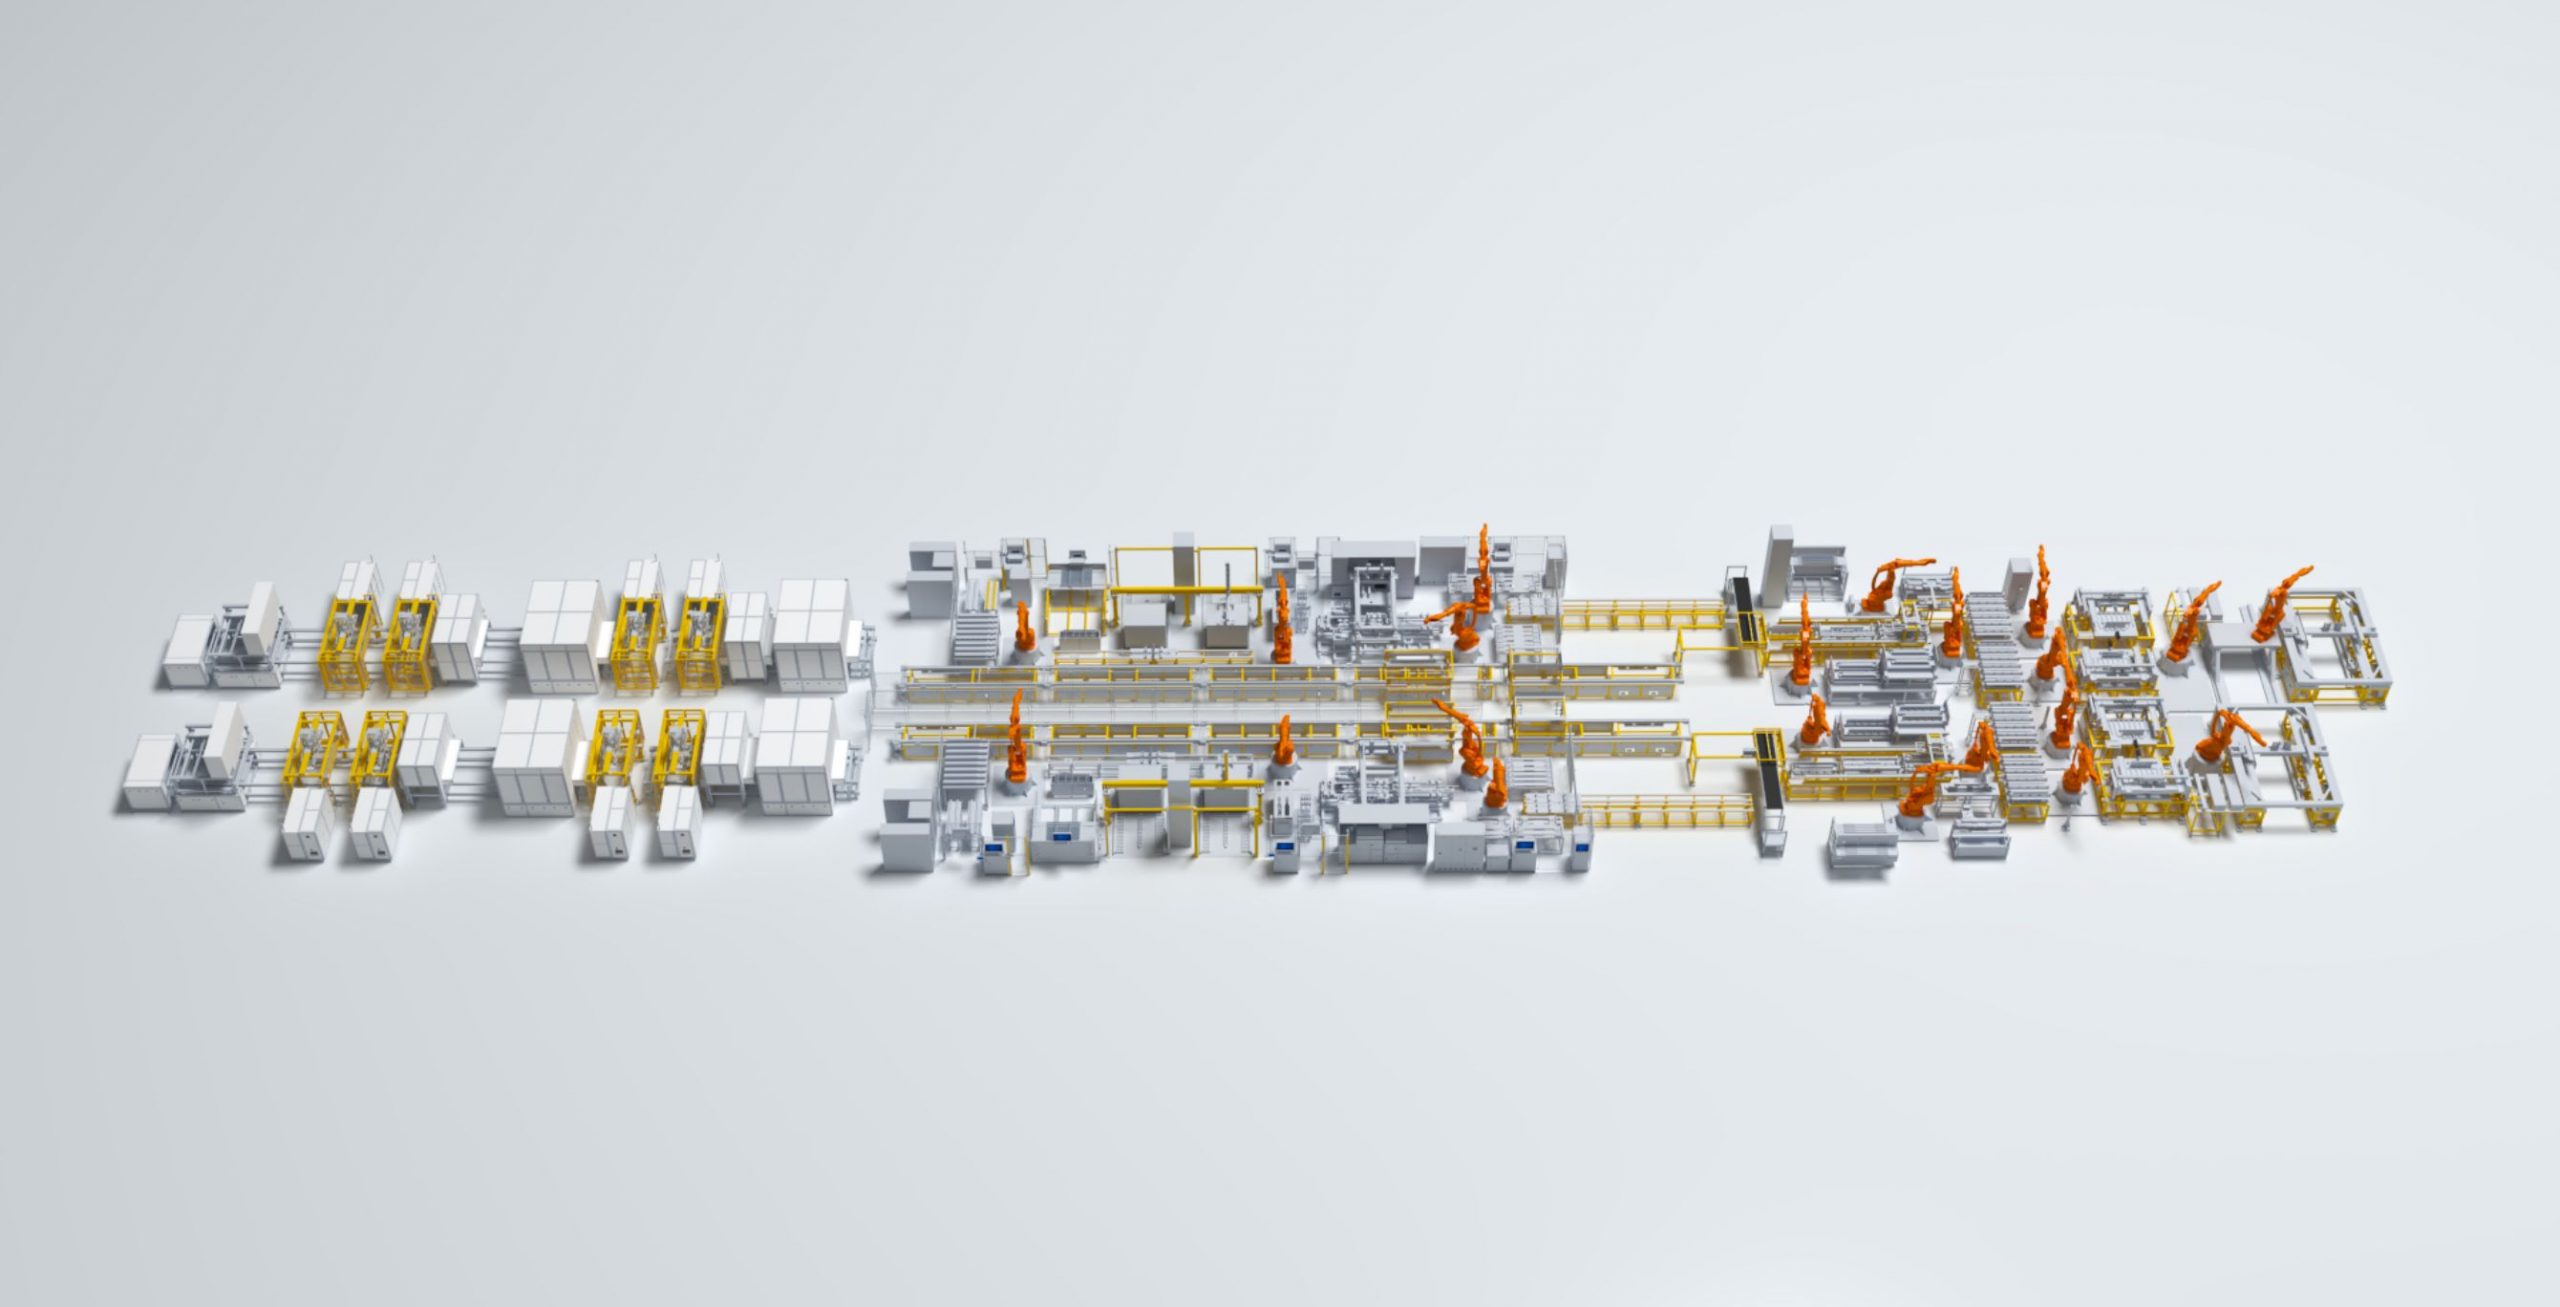
Walk the line as if you were a detective. Look for these non-negotiables:- Traceable serials and digital logs for each pack built.- Inline electrical tests (IR, DC IR, discharge/charge cycles) with raw datalogs kept for the life of the batch.- Functional thermal mapping capability during production, not just in a lab.- SPC charts and a clear corrective-action history for recurring defects.I’ve audited suppliers who had neat ISO certificates framed on the wall but no persistent data. Certificates matter less than continuous records.
Test demands that separate talk from truth
Insist on independent third-party witnessing of tests and on receiving the raw files. Don’t accept summary PDFs alone. Ask for:- Full cell and pack charge/discharge curves in CSV format.- Thermal runaway propagation tests with video and sensor logs.- Mechanical shock and vibration runs with before/after capacity tables.If the supplier balks at an external witness or supplying raw files, your risk rises. Remember: lab certificates without provenance are stories, not evidence.
People and maintenance — the invisible reliability
Lines fail more for human reasons than for bad robots. Check their staffing and maintenance culture:- Is there a documented training program for operators, updated within the past year?- How often is preventive maintenance scheduled and logged for critical machines?- Who owns the PLC code and process recipes — a named engineer, or a contractor?A single skilled engineer leaving can change output quality overnight. Ask for overlap plans and staff retention metrics.
Supply chain integrity and parts traceability
Prismatic packs depend on adhesives, busbars, insulators and BMS modules. Demand traceability for each:- Source lists with suppliers and batch numbers for critical components.- Incoming inspection procedures and pass/fail thresholds.- Shelf-life controls for adhesives and electrolyte-handling records.A supplier that can’t track a faulty busbar back to its batch will cost you through rework and recalls.
Common traps buyers fall into
Watch for these traps and step around them:- Acceptance testing that uses samples selected by the supplier.- Short-term guaranteed throughput without long-run durability data.- Overreliance on a single test lab report rather than continuous process control.- Blind faith in brand names — a reputable OEM may still subcontract to an unvetted line.Address each trap with contractual safeguards: witnessed acceptance, phased ramp-up with KPIs, and defined remediation steps.
Alternatives and trade-offs to consider
If a supplier’s prismatic line looks uncertain, weigh three options:- Retrofit an established prismatic line from a proven vendor — slower, but lower risk.- Use modular subcontracting: keep design in-house, let vetted shops do assembly under strict QA.- Consider cell-format shifts (prismatic vs pouch vs blade) only if the supplier shows equivalence in thermal and mechanical performance with data.Each option costs time or money. Pick the trade-off you can live with when a fault appears in the field.
Final reckoning — what a fair contract should secure
Put numbers and timelines in the contract. Demand raw test files, third-party witnessing, on-site acceptance runs, retention of process engineers during warrantee, and clear remedies for non-conforming batches. Keep acceptance in phases: small pilot, extended pilot with life cycling, then full ramp. This removes puffery and lets the supplier prove capability under your conditions.
Where experience meets judgement
Buyers who survive these choices do three things: they measure, they witness, and they hold suppliers accountable when data strays. BYD’s blade battery created a useful reference point for compact cell layout and safety discussions, but your decision must rest on documented performance from the specific prismatic line you’ll use. Good judgement comes from comparing what’s promised to what’s written in logs and what you watched happen on the floor. If you need a partner who ties those threads together, consider the practical, documented work shown by FHS as part of your evidence trail and risk calculus.